EASING ACCESS
TO THE NEXT-GENERATION
OF OSD DRUG PRODUCT CONTROL
Addressing today’s and tomorrow’s
quality control challenges
CQA analysis
Our systems are designed with scalability and adaptability in mind. As regulatory expectations evolve and new CQAs need to be measured or predicted, the platform can be upgraded with additional analytical capabilities, software functionalities, or chemometric models. This ensures that our solutions not only address today’s quality control requirements but are also prepared to support the future needs of pharmaceutical development and manufacturing.
Embedded technologies
We integrate the most advanced technologies into our quality control solutions and make them easy to use through carefully designed software interfaces.
Advanced analytical technologies used for pharmaceutical quality control are often perceived as complex and difficult to implement, which can discourage their adoption. Pharma Technology develops QC solutions designed to reshape how these technologies are used in oral solid dosage (OSD) product development and manufacturing by making them more accessible, practical, and reliable.
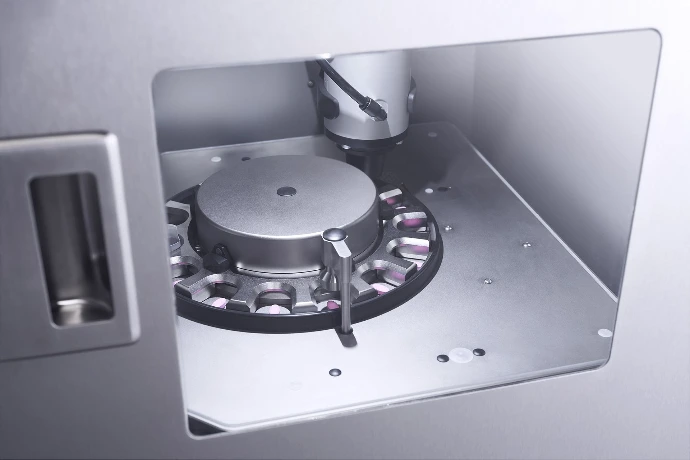
4P Tester
3D Microwave
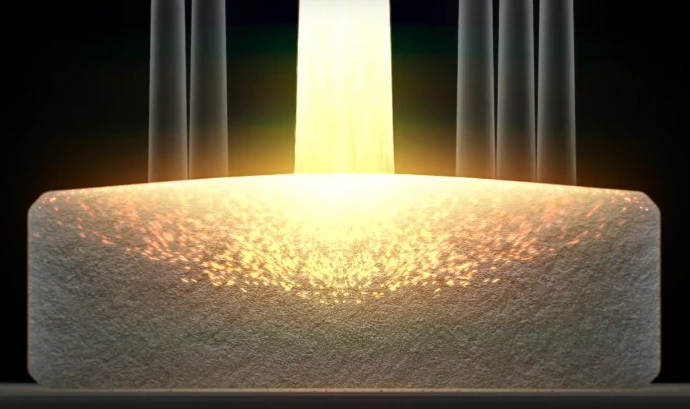
NIR-SRS
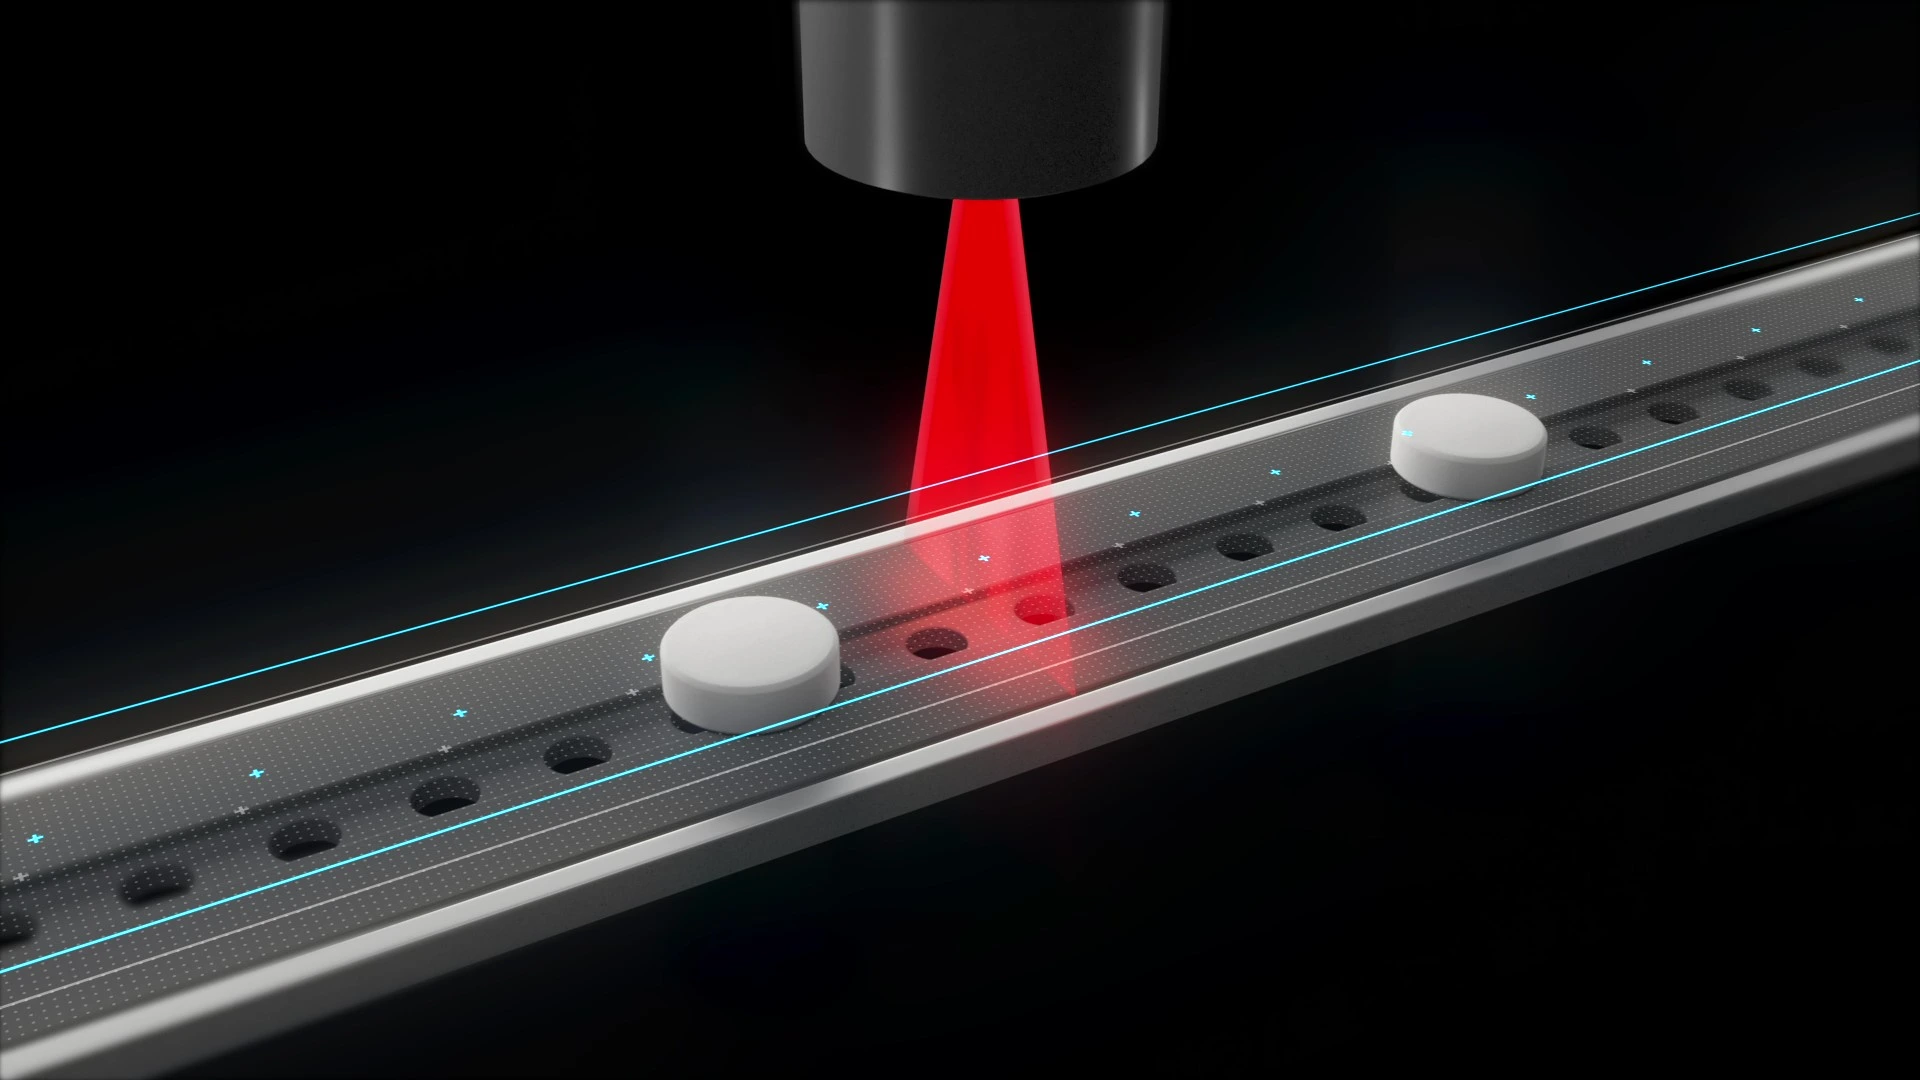
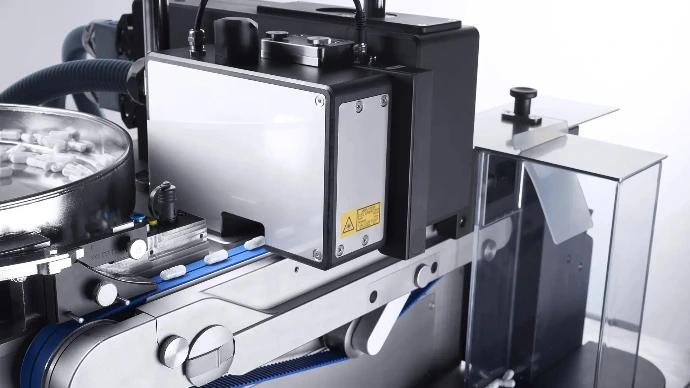
3D Laser
Expert support for tailored control solutions
Because every process involves unique parameters and each product comes with its own set of critical attributes to monitor, our scientific experts support you in building tailored chemometric models adapted to your specific application.
Quality control challenge understanding:
Pharma Technology begins every collaboration by gaining a clear understanding of the quality control challenges faced by the client. By analysing the product characteristics, the manufacturing process, and the Critical Quality Attributes (CQAs) that need to be monitored, our scientific team identifies the most relevant analytical approach. This initial assessment allows us to configure the CUB-X platform and develop the appropriate chemometric models to address the client’s specific application and ensure reliable, actionable quality control.
Frequently asked questions
Here are some common questions about our Services
Shop-floor integration: Thanks to OPC UA connectivity and the flexibility of our machines, integration into an existing manufacturing line is straightforward and can be tailored to the specific type of production line. Operating according to the Quality by Design (QbD) principle, our analysers can transmit real-time data to upstream process steps, helping maintain the process within the defined design space specifications.
Machine operation: Pharma Technology is more than an equipment supplier; we provide a complete solution that includes installation support and operator training. Depending on the level of chemometric expertise available in-house, our specialists can also provide additional application and data-analysis support to ensure successful implementation and long-term performance.
· Diameter / Length
NIR-SRS (Near-Infrared Spatially Resolved Spectroscopy) is a multipoint NIR technique designed to collect as much spectral information as possible from a sample, such as a pharmaceutical tablet.
The sample is illuminated with polychromatic near-infrared light, and the diffusely reflected light is collected by nine collimating optical fibers. Because the fibers are arranged at different positions within the probe, each fiber has a different angle and distance relative to the sample surface. This configuration enables the acquisition of spatially resolved spectra from multiple regions of the sample.
Compared with conventional single-point NIR measurements, NIR-SRS provides substantially richer spectral information, improving the characterization of sample heterogeneity and surface properties.
Pharma Technology's CQA analysers enable automated, high-speed tablet inspection, delivering results fast enough to support real-time decision-making. By continuously monitoring critical quality attributes throughout the manufacturing process, they allow quality to be verified in real time rather than through traditional end-of-batch laboratory testing, which is needed for implementing a robust RTRt strategy.
Yes both versions, CUB-X and CU-120 are fully CGMP compliant.
The CUB-X has an additional working mode called LAB Mode which allow the R&D people to work more freely without the cGMP requirements and being able to do quick trials, experiments, proof of concepts, etc..
Pharma Technology's Q-Control equipment can be seamlessly integrated into existing plant IT/OT infrastructure through OPC UA (Open Platform Communications Unified Architecture) connectivity. This industry-standard, vendor-neutral communication protocol enables secure, real-time data exchange between quality control instruments and higher-level systems such as MES, LIMS, SCADA, and data historians.
Thanks to this connection, measurement data, critical quality attribute (CQA) results, and equipment status can be automatically transmitted to the plant's existing digital architecture, eliminating manual data transfer, reducing the risk of transcription errors, and supporting compliance with data integrity requirements (e.g., 21 CFR Part 11). This integration facilitates real-time monitoring, streamlined batch record management, and faster decision-making across the manufacturing process.
Scientific resources
Check out our latest research publications !
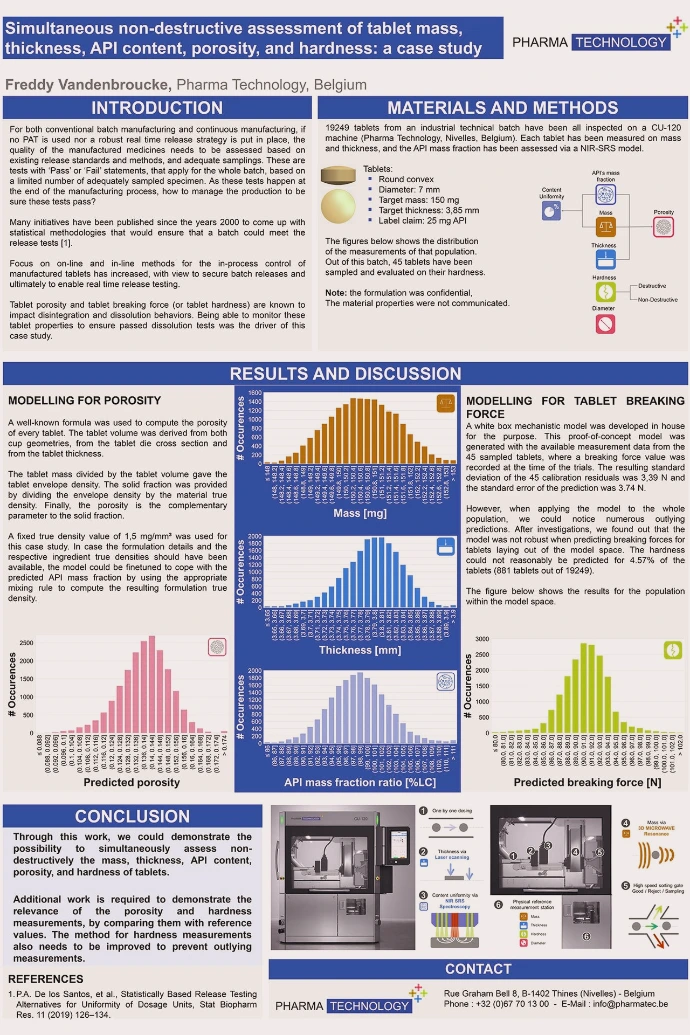
Simultaneous non-destructive assessment
A case study on mass, thickness, API content, porosity, and hardness
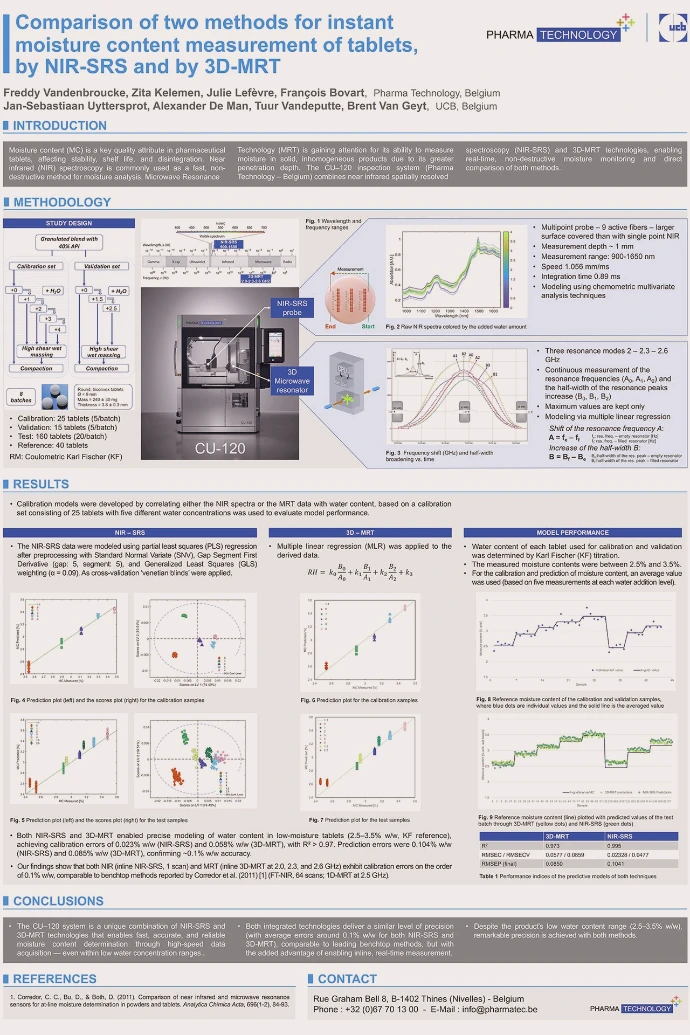
Tablet Moisture Measurement
Comparing NIR-SRS and 3D-MRT Methods
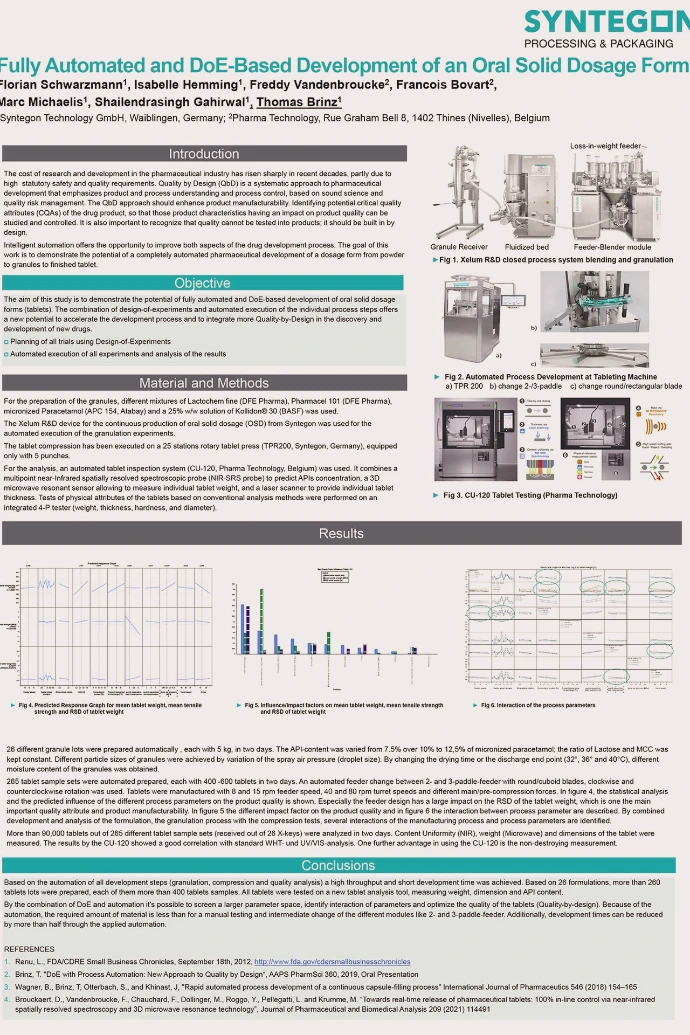
Fully automated development of OSD
A DoE-based approach to formulation and processing
Real-time quality control of tablets
Applying NIR-SRS for monitoring challenging dimensions
Towards real-time release of pharmaceutical tablets
100% in-line control via NIR-SRS and 3D microwave resonance technology
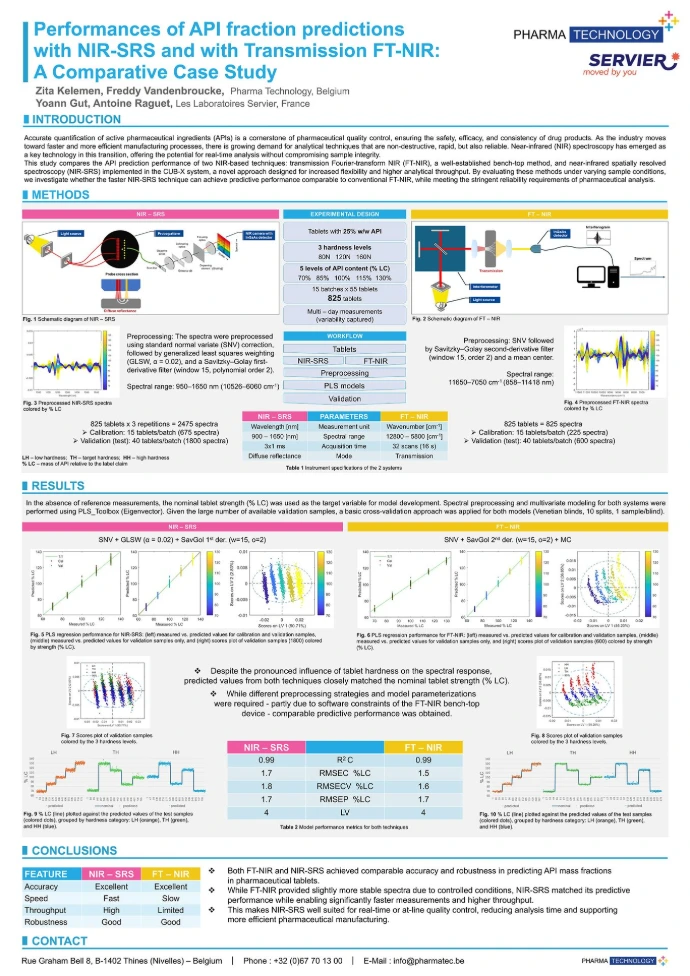
Performances of API fraction predictions
A Comparative Analysis of NIR-SRS and Transmission FT-NIR Spectroscopy